Product definition
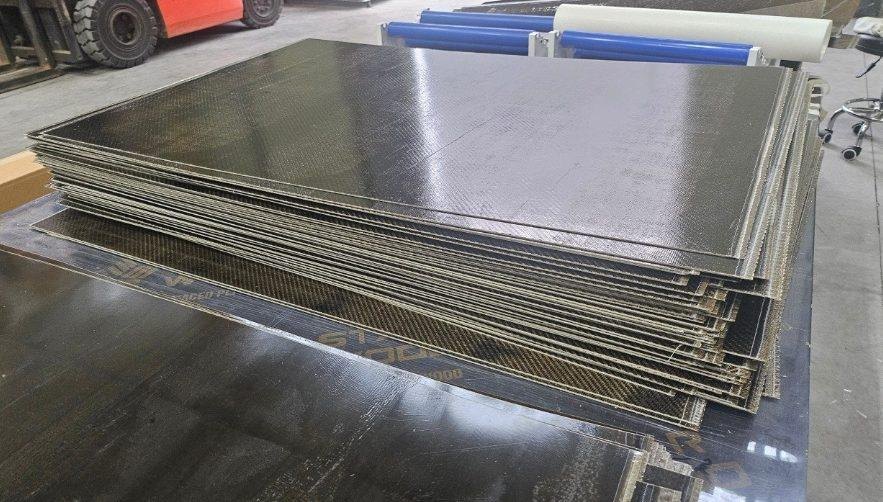
A multi-ply consolidated structural sheet produced by heating, compacting and cooling thermoplastic fabric prepreg. Material selection and layup design connect to prototype development.
 한국어
THERMOPLASTIC COMPOSITES
Thermoplastic Laminate
Carbon · Basalt · Glass / Elium®
CARO MATERIALS Thermoplastic Laminate
A multi-ply consolidated structural sheet produced by heating, compacting and cooling thermoplastic fabric prepreg. Material selection and layup design connect to prototype development.
THERMOPLASTIC ADVANTAGES
Less expiry management · Shorter subsequent forming · Continuous production and automation
| Comparison | CARO thermoplastic prepreg / laminate | Typical thermoset prepreg / laminate |
|---|---|---|
| Storage and expiry | Fully polymerized solid prepreg requires no refrigerated or frozen storage and has no expiry caused by the progress of uncured-resin curing. | Uncured prepreg requires resin-specific shelf/out-life management and may require cold storage. The same uncured-resin expiry concept does not apply to fully cured laminate. |
| Subsequent forming principle | Already polymerized material is heated, consolidated/formed and cooled, without waiting for a separate resin cure at this stage. | Prepreg layup requires chemical resin curing; post-curing may be included depending on the system. |
| Processing time | Eliminating the cure wait in subsequent forming supports shorter cycle design. Actual time depends on thickness, heating and cooling. | Cure time and sometimes post-cure time are required. Rapid-curing thermoset systems also exist; comparisons must be process-specific. |
| Continuous production and scalability | Roll-prepreg feeding, continuous CCM laminate manufacture, automatic cutting and press automation support repeatable production. | Cure conditions and material out-life must be incorporated into planning. Thermosets can also support automated, continuous and high-volume processes. |
| Inventory and handling | Avoids cold-storage and thawing requirements; tack-free handling supports storage, feeding and layup. | Prepreg may require cold-chain logistics, thawing and out-time tracking. Cured laminate follows separate handling requirements. |
| Thick laminates | No cure exotherm must be controlled during heated consolidation. Thick sheets are reviewed in a separate press for heat transfer, pressure and cooling. | Cure exotherm and heat transfer inform the cure schedule. Thick sheets are possible, with appropriate process control. |
| Changes after forming | Reheating and reforming can be considered under material- and structure-appropriate conditions. | Cured resin is difficult to reform through reheating in the manner of a thermoplastic. |
| Recycling | Thermoplastic behavior supports consideration of reprocessing and recycling routes. | The cured crosslinked matrix does not readily remelt; separate recycling routes are required. |
The expiry statement applies to already polymerized CARO products, not to the storage life of liquid Elium® resin before manufacture. Moisture, contamination, UV and heat exposure remain storage considerations.Comparisons describe general principles and depend on the resin and process.
Technical references: Hexcel · Prepreg Technology · Arkema · Elium®
KEY FEATURES & BENEFITS
Consolidated multi-ply sheets support subsequent forming and structural-component development.
Continuous CCM production at 1,000 mm width supports cut-to-length and narrower-width supply. Thick sheets are reviewed for separate press processing.
Fiber reinforcement and layup design support lightweight structures with the strength and stiffness required for the application.
Thermoplastic resin enables subsequent forming and reforming to be considered under appropriate heating conditions.
Fiber, resin and layup choices can address impact and damage requirements. Performance is verified for the specific application.
Resin and structural choices are reviewed for suitability under chemical exposure and service-temperature conditions.
Thermoplastic materials support consideration of recycling, reprocessing and repair routes, selected according to the product structure and conditions.
Already polymerized prepreg is heated and consolidated into products, with routes to continuous consolidation and press forming.
Carbon, Basalt and Glass materials, plain and twill fabrics, thickness and layup are reviewed for the intended product.
Material use, layup, manufacturing processes and automation are considered together to improve development and production cost efficiency.
Actual performance and benefits depend on materials, layup, processing and the service environment.
Our CCM line produces sheets up to 1,000 mm wide, with a typical thickness range of 0.2–3.0 mm. Sheets are automatically cut to the requested length and can be trimmed to narrower widths.
Thicker sheets, such as 15 mm or 20 mm, are reviewed for separate heated press consolidation. Continuous production is constrained by unwinder and ply capacity. Rotated ply orientations are reviewed for separate press processing, not continuous CCM production.
Heated consolidation of already polymerized thermoplastic prepreg is distinct from thermoset curing. Thick-sheet conditions require review of heat transfer, pressure and cooling.Hole and contour machining are not included in standard supply.
CCM LAMINATE SPECIFICATIONS
| Item | Specification / confirmation status |
|---|---|
| Manufacturing width | 1,000 mm |
| Normal thickness range | 0.2–3.0 mm · subject to specification and process review |
| Supply length | Customer-specified set length → automatic cutting |
| Narrow-width supply | Narrower-width cutting available when required |
| Custom thick sheets | 15 mm, 20 mm and other thick sheets: separate heated press consolidation, outside the continuous CCM specification |
We review materials, layup, thickness and forming options against your application requirements and support prototype development.
Explore Prototype Development →